01
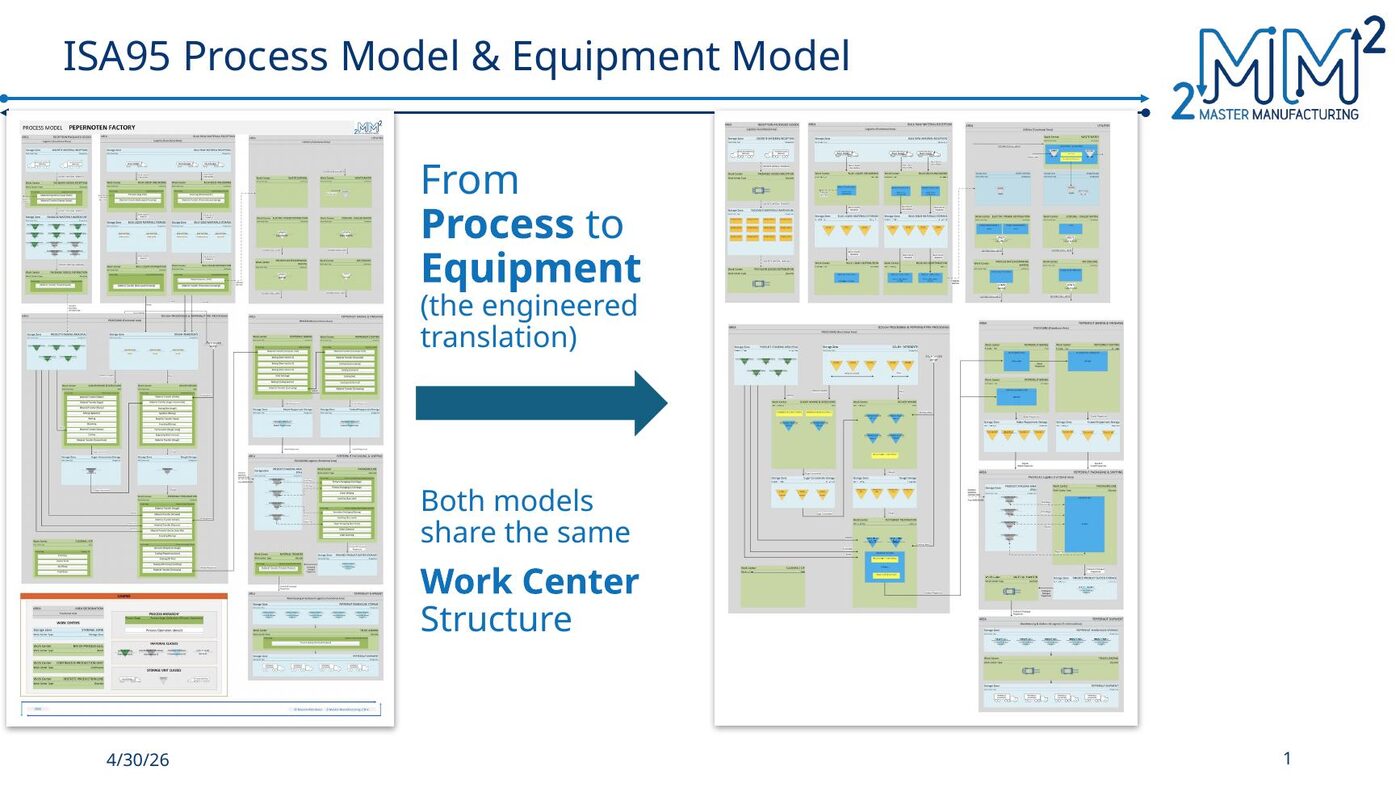
From process to equipment
We first model what the factory does (the process model), then translate it into what it is built from (the equipment model). Both share the same work center structure.
Approach
01
We first model what the factory does (the process model), then translate it into what it is built from (the equipment model). Both share the same work center structure.
02
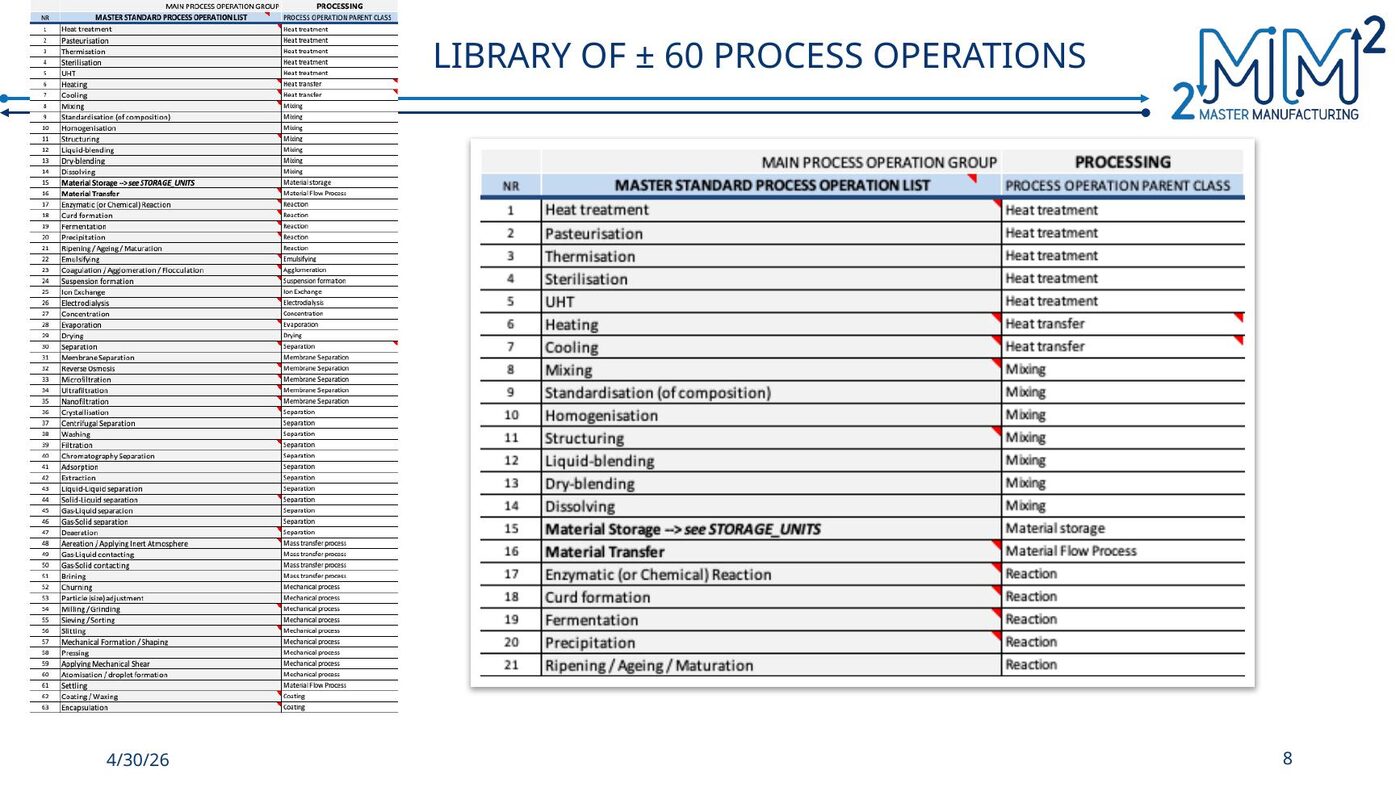
Built on the unit operation concept that founded chemical engineering at MIT in 1920. Mixing, heat treatment, separation, drying, storage — every factory is a combination of these.
03
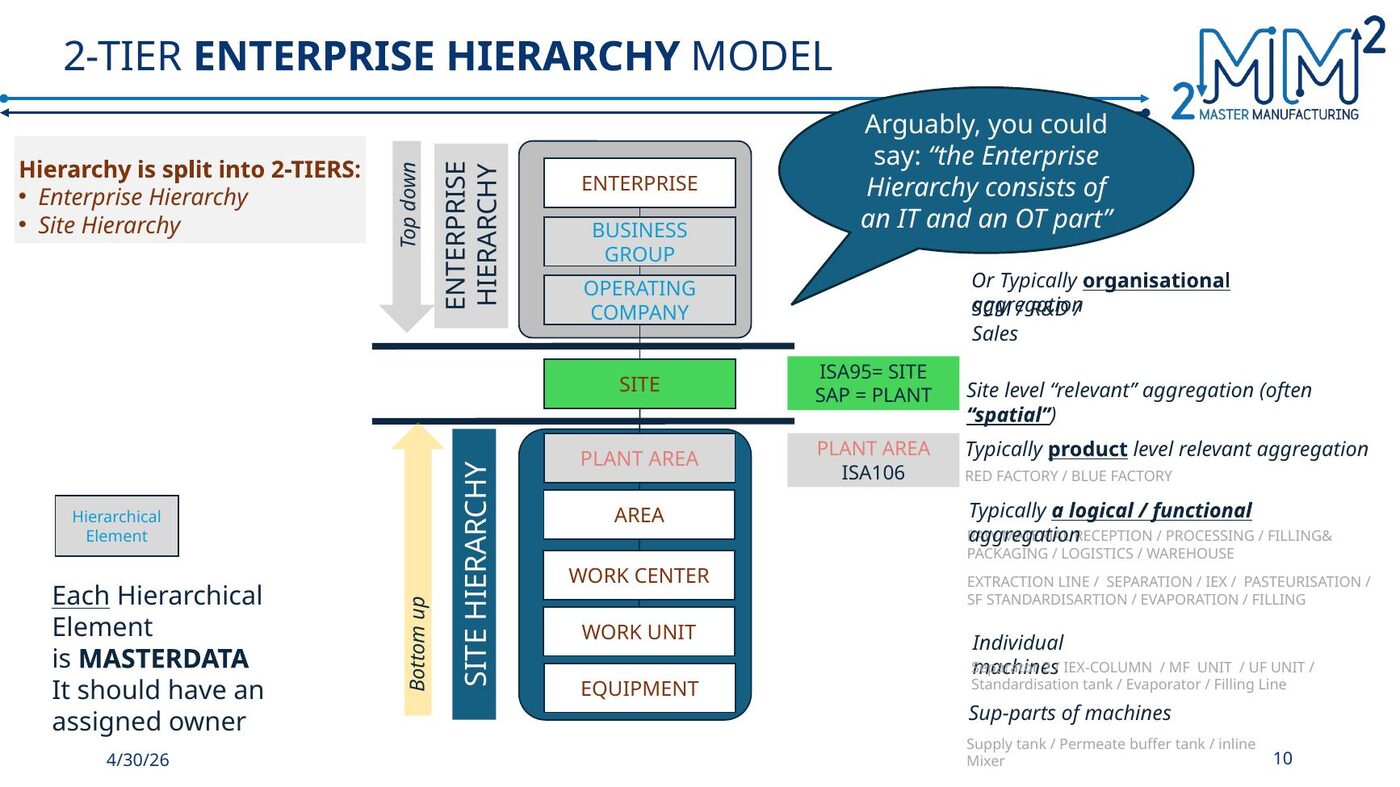
An enterprise hierarchy (top-down, organisational) and a site hierarchy (bottom-up, physical), meeting at the site — which ISA-95 calls a Site and SAP calls a Plant.
04
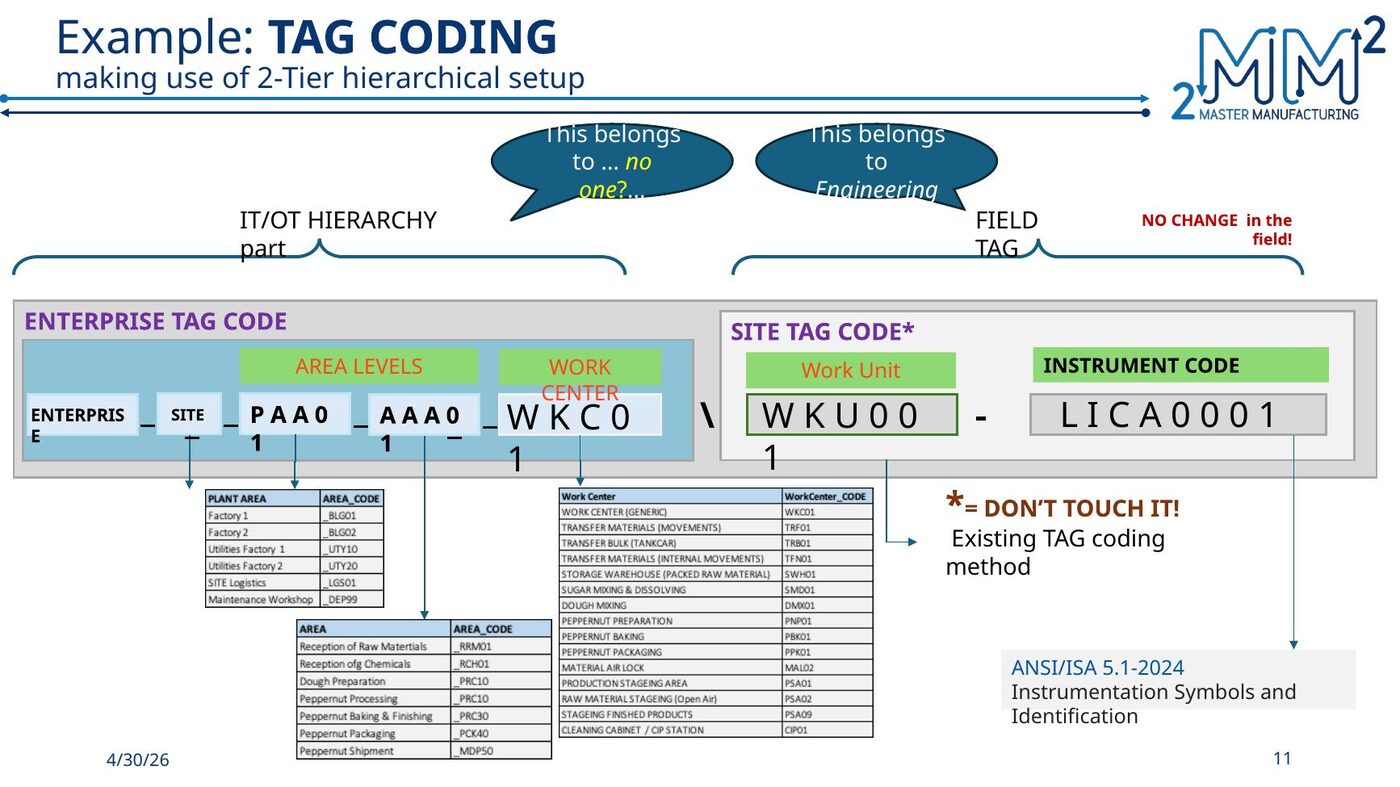
The IT/OT hierarchy is prefixed to existing field tags. Engineering keeps its instrument codes; data gets full context for your historian and UNS.
05
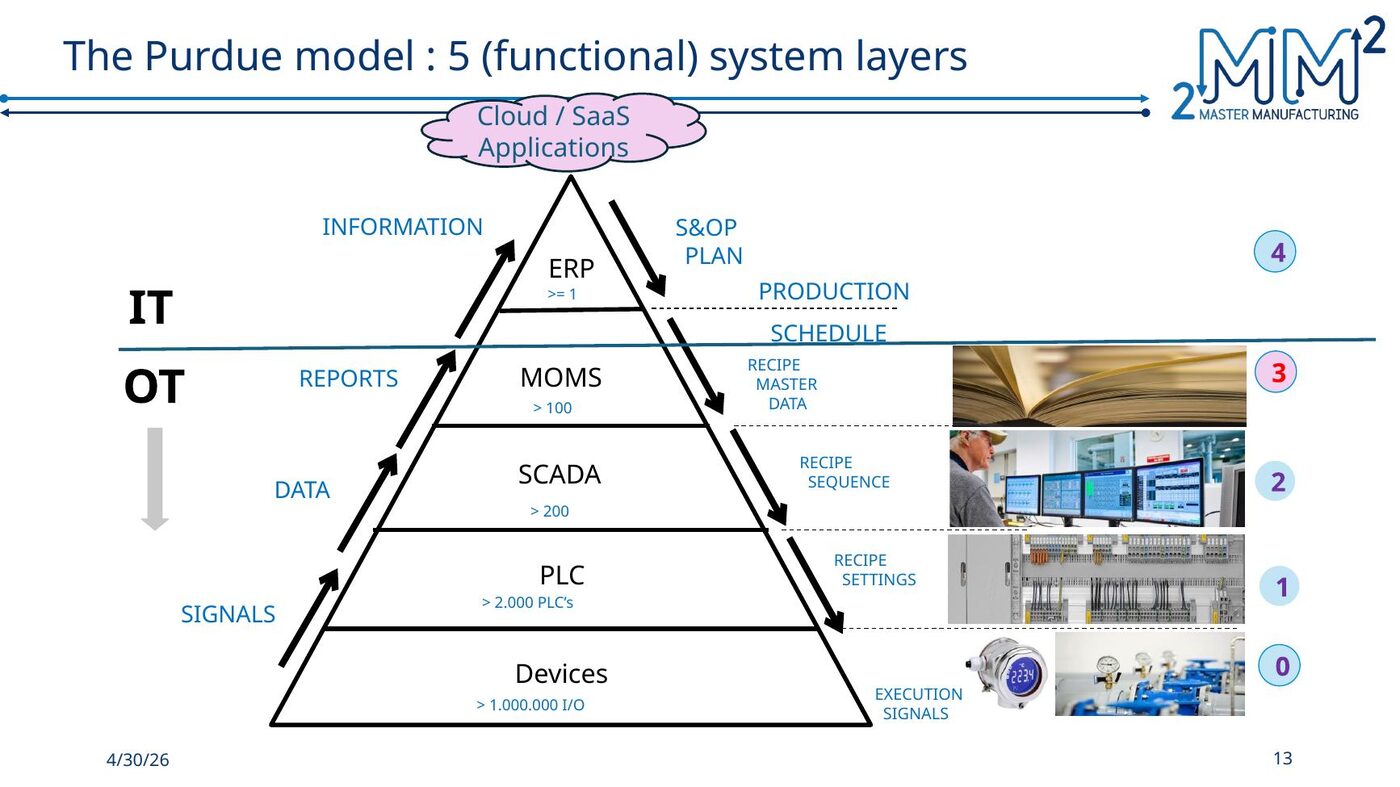
From devices and PLCs through SCADA and MOMS up to ERP: one shared language between signals, data, reports and information.
TAG coding method v2.0
One tag structure, every site, one data lake. Each part of the tag has exactly one meaning and one fixed format, so "all baking lines across all sites" becomes a single query.
01 · AAA
NIX
Site
Mandatory in the data lake. One corporate list of unique 3-letter site codes.
02 · AAA
PPN
Plant
Plant within the site. Joined to the site with a dot.
03 · nAAA
1RWH
Area
Area number 1–9 + 3-letter code. Same meaning at every site.
04 · AAAnn
TRD01
Work Center / Unit
Standard work-center types, numbered 01–99.
05 · AAAnn
PST01
Equipment
Equipment module within the unit. Copy-paste units keep their structure.
06 · ISA 5.1 + nnn
FT101
Instrument
ISA 5.1 function letters, 100-number range per Work Unit.
07 · -nn
-01
Component
Optional, for replaceable parts and spares.
Two forms, one tag
Short form on drawings and in the control system; full form with SITE.PLANT. added automatically when data leaves the plant.
Fixed separators
Dot for the site prefix, underscore inside the plant, slash generated for UNS topics.
Equipment ≠ process
Equipment tags and process-step codes live in separate code lists, never mixed.
No enterprise in the tag
The enterprise is always the same in one data lake; it lives in the UNS root.
Three automatic checks
Every tag is unique, follows the format, and has an existing parent.
Publish as UNS
Final step: each tag becomes a topic, e.g. enterprise/nix/ppn/1rwh/trd01/pst01/ft101.
ERP meets Level 3
Administrative ERP processes only become reliable when they are anchored to the physical factory. We map your global business processes onto the ISA-95 equipment hierarchy and process segment model, so finance, planning, maintenance and quality all speak the same structure as the shop floor.
Order to Cash
Demand to Supply
Plant Maintenance
Quality
Finance to Manage
| ISA-95 level | Tag | ERP object | Business processes |
|---|---|---|---|
| Enterprise | NIX | Company code / legal entity | Consolidation, Chart of Accounts |
| Site | NIX.PPN | Plant | MRP, S&OP, Stock control |
| Area | …5BKF | Profit center / cost center group | Cost allocation, Reporting |
| Work Center | …5BKF_OVN01 | Cost center + ERP work center | Production orders, Routings, Scheduling |
| Work Unit | …OVN01_TNL01 | Fixed asset + functional location | Maintenance, Depreciation, CAPEX |
| Equipment Module | …TNL01_BRN01 | Maintenance equipment / BOM | Notifications, Spare parts |
01
Link matrix
Every business process anchored to the ISA-95 level where it actually happens.
02
One tag, one key
The equipment tag doubles as cost object, asset number and maintenance location.
03
Process Segments as bridge
ERP routing steps become ISA-95 process segments, executed on Work Centers and Units.
04
Level 4 ↔ Level 3
Planning, order and cost in ERP; scheduling, execution and data collection in MOM.
05
Transactions as UNS events
Order start, inspection lot or maintenance notification published under the tag.
A free 30-minute intake call to map where your factory stands.